Hey there, it’s Jake from [Your Company Name], and I get it—when you’re in the market for a bridge machining center, the first question that pops up (after, like, “how much is this gonna cost?”) is “what’s the max cutting speed?” I hear it all the time, from job shop guys with a stack of aluminum parts to aerospace guys working on titanium alloys, and honestly? It’s not a one-word answer. A lot of companies will slap a random number on their spec sheet, but that’s useless unless you know the context behind it. Let’s break this down like I’m talking to a buddy who’s got a shop full of messy parts and a deadline next week. Bridge Machining Center Machine
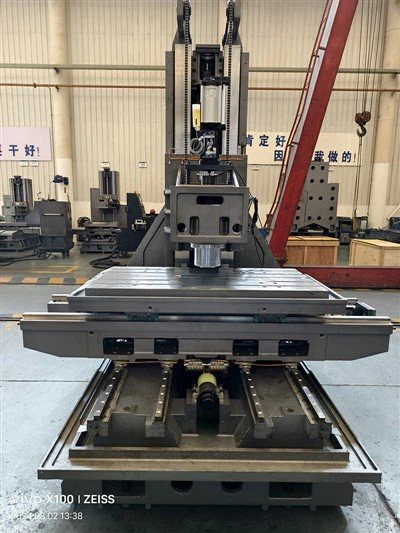
First off, let’s define what we’re even talking about here. A bridge machining center—you know, that gantry-style machine that’s perfect for big, long parts you can’t fit on a vertical mill? It’s got a moving gantry, a stationary table (sometimes, depending on the setup), and a spindle that zips around X, Y, Z axes. Cutting speed, for the uninitiated, is how fast the tool moves relative to the material you’re cutting—usually measured in surface feet per minute (SFM) or meters per minute (m/min). Max cutting speed isn’t just how fast the spindle can spin, though. It’s a whole mix of factors, and if you ignore any of them, you’re gonna either burn up a tool, crash the machine, or worse.
Let’s start with the big one: spindle speed. Most of our bridge machining centers run with spindles that top out anywhere from 10,000 RPM to 25,000 RPM, and some high-torque specialty ones hit 40,000 RPM if you’re dealing with small, high-precision tools. But wait—RPM alone don’t equal max cutting speed. If you’re using a ½ inch end mill, your surface speed is way different than if you’re using a 2 inch face mill. The formula is simple: SFM = (π × diameter × RPM) / 12. Do the math, and you’ll see why a ½” end mill at 10,000 RPM is doing ~1,308 SFM, while a 2” face mill at the same RPM is only ~5,236 SFM. That’s a huge gap, so that spec sheet number you saw? It’s probably the theoretical max based on the smallest tool and highest RPM, not what you’ll actually use for most jobs.
Next up: material. This is where 90% of the “max speed” lies. Let’s be real—you’re not cutting titanium at the same speed you cut 6061 aluminum. If you’re machining aluminum, which is soft and doesn’t generate a ton of heat, you can run those SFM numbers way high. We regularly get our bridge centers cutting aluminum at 2,000 to 4,000 SFM, sometimes even higher for thin, delicate parts where heat buildup is bad. But switch to stainless steel? Now you’re down to 100 to 300 SFM. Titanium? Oh, that’s a slow burn—maybe 50 to 150 SFM, and you better have a good coolant system, or you’ll see tool wear in 2 minutes flat. And forget about hardened steel (HRC 50+)—you’re looking at 30 to 80 SFM, max. So if someone tells you their bridge center does 10,000 SFM, ask them what material that’s for. It’s probably aluminum, and that’s not gonna help you when you’ve got a batch of 304 stainless valves.
Then there’s the machine itself. Not all bridge machining centers are created equal. The linear guides vs. box ways thing is a big one. Linear guides are smoother, let the axes move faster, so you can get higher feed rates and keep up with that spindle speed. Box ways are stiffer, which is great for heavy cuts, but they’re slower. Our top-of-the-line bridge centers use high-precision linear drives on all axes, so the machine can actually keep up with what the spindle is doing—no lag, no vibration. If you buy a cheap import bridge center, the linear motors might not be tuned right, so even if the spindle hits 20,000 RPM, the axis can’t move fast enough to translate that into actual cutting speed, and you’ll get chatter marks all over your part. Also, the spindle power matters. A 10 HP spindle can’t push that ½” end mill as hard as a 20 HP spindle, so you might have to slow down to avoid bogging the motor down. We test every spindle on our machines in real job conditions, not just lab tests, so we know exactly what they can handle without dropping power.
Coolant and tooling round out the list. If you’re running flood coolant, you can push speeds a bit higher because it carries heat away. Through-spindle coolant (TSC)? Game changer. That high-pressure coolant blasts right at the cutting edge, so you don’t get built-up edge (BUE) on the tool, especially with aluminum. We recommend TSC on all our high-speed bridge centers, and our optional TSC system can go up to 1,000 PSI, which makes a huge difference in tool life and speed. Then there’s the tool holder. If you’re using a CAT 40 holder, that’s fine for mid-range speeds, but for high RPM, you need a HSK-A63 or a CAPTO holder, which are more rigid and balanced. Unbalanced holders will cause vibration at high speeds, and that vibration will ruin your cut and wear out the spindle. We work with tooling suppliers to set up balanced tool packages for our machines, so customers don’t have to figure that out on their own.
Wait, let’s talk about real-world examples, because that’s what matters. Last month, we had a customer who makes custom RV chassis parts—big, 10 foot long aluminum beams. They were using a competitor’s bridge center, and they could only run at 1,800 SFM, so their cycle time for each beam was 45 minutes. They switched to our machine, and with the right tooling and TSC, we got them up to 3,200 SFM. Now their cycle time is 22 minutes, same part, same tool. That’s the actual max cutting speed they care about—not some theoretical number. Another customer does titanium aerospace brackets. They needed precision, so we dialed their max speed to 120 SFM, but upped the feed rate to make up for it, and they’re hitting their tolerance specs (±0.0005”) way faster than before.
I should also address the myth that higher speed = better. No, that’s not how it works. If you push your max cutting speed too high, you’ll get excessive tool wear, or the tool will break, or the part will distort from heat. Or worse, the machine will vibrate so bad it’ll throw off the alignment. We always work with customers to find the sweet spot—max speed that’s balanced with tool life, part quality, and cycle time. Our machines are set up to let you adjust that easily, with touchscreen controls that give you real-time feedback on spindle load, temperature, and vibration, so you don’t have to guess.
So what’s the takeaway here? The max cutting speed for a bridge machining center isn’t a static number. It’s dependent on spindle speed, material, tool type, machine rigidity, coolant, and even the operator’s setup. For our premium bridge machining centers, the theoretical max (for small aluminum tools) is around 6,000 SFM, but the practical max for most jobs is 1,500 to 4,000 SFM—way higher than the import brands we see cutting corners. If you’re working with harder materials like stainless or titanium, that drops, but our machines still outperform others because of the rigid design and high-torque spindles.
Look, at the end of the day, we’re not just selling a machine. We’re selling a solution to your production headaches. If you’re tired of cycle times dragging, parts coming out with bad surface finish, or machines that can’t keep up with your jobs, let’s chat. We can walk you through your specific parts, materials, and deadlines, and figure out exactly what max cutting speed you need—not some random spec number. No pressure, no sales pitch—just honest talk about what’ll work for your shop.
If you wanna learn more, just reach out. We’ve got case studies, real customer data, and a team that knows this stuff inside and out. Let’s get your production moving faster.
5 Axis Machining Center References:
- Machining Data Handbook, 4th Edition. Society of Manufacturing Engineers, 2020.
- “Bridge Type Machining Centers: Design, Performance, and Applications.” Modern Machine Shop, 2022.
- Tooling Solutions for High-Speed Machining. Kennametal Inc., 2021.
Smartech Machinery & Equipment Co., Ltd.
As one of the most professional bridge machining center machine manufacturers and suppliers in China, we also support customized service. Please rest assured to buy bulk bridge machining center machine made in China here from our factory. Contact us for more details.
Address: Room 2832, Changping Commercial Mansion, Shihua Road, Futian Free Trade Zone, Shenzhen, China
E-mail: smartech@smartechcnc.cn
WebSite: https://www.smartech-cnc.com/
