Hey folks, if you’ve ever worked with a nut former—whether you’re a seasoned production manager, a new maintenance tech, or just someone who’s ever stared at a half-formed batch of nuts and thought “what even broke here?”—you know how frustrating it is when a machine goes down mid-run. As someone who’s been supplying nut formers for over a decade, I get it more than most. The last thing you need when you’re cranking out batches for your biggest client is a part that’s NLA (no longer available) or that costs half as much as the machine itself. Today we’re breaking down the actual replacement parts you’ll actually need for a nut former—no clickbait, no jargon that makes your eyes cross, just real stuff we see every week on our service line. Nut Former
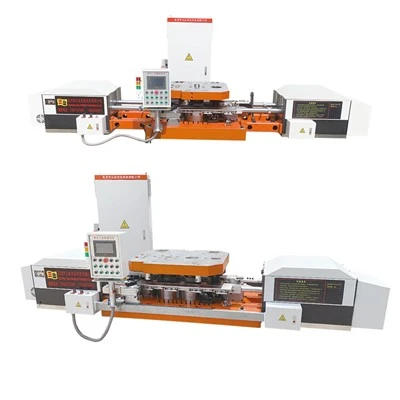
First, let’s keep this simple: a nut former’s whole job is to take that raw, usually roasted nut (think almonds, peanuts, cashews, whatever your thing is) and turn it into a uniform shape—whether that’s a circle, a square, a football for game day snacks, or even those fancy textured shapes for premium brands. The machine runs on a mix of metal parts, small components that move nonstop, and stuff that touches the food, so parts break for two main reasons: wear and tear, or just regular use. You don’t replace a nut former’s control panel every month, obviously, but the parts that touch the nuts or move back and forth 50 times a minute? Those are your regular replacement parts.
Let’s start with the workhorses—this is where 90% of our replacement orders come from. First up: the die set. Wait, not just any die set—this is the pair of metal plates that actually squeezes the nut into shape. The top die pushes down, the bottom die has the matching cavity, and that’s where the magic happens. Dies wear out because over time, the constant pressure from metal and sometimes (rarely, but it happens) a stray rock or chunk of shell that slips through the pre-cleaner will nick, scratch, or dull the cavity. Scratched dies mean uneven nut shapes, and if the nick is bad enough, you might get split nuts or even nuts that get stuck and jam the machine. Good thing is, we make die sets in every shape and size you could ask for—no generic parts here, just custom fits for whatever model nut former you’ve got. Pro tip: if you run high-volume (like 24/7 snack production), swap your die set every 3-6 months as part of scheduled maintenance, not just when it breaks. We’ve seen plants that wait till dies are shot and end up with 2 hours of downtime instead of a 15-minute swap.
Next on the workhorse list: the punch assembly. That’s the part that hits the die, right? It’s the round (or shaped) metal rod that does the actual squeezing. Punches take a beating every time they stamp down. They can bend, develop wear on the tip, or even break off if something hard gets in the machine. We’ve had customers send back punches that look like they got run over by a forklift (okay, maybe not that bad, but close) because they skipped cleaning out their feed hopper. A loose shell chunk can get wedged between the punch and die, and bam—next thing you know, your punch is misaligned and your nuts are shaped like random blobs. The punch assembly usually comes with a guide pin too—don’t sleep on that. The guide pin keeps the punch straight, and over time, it can wear so the punch wobbles, leading to misshapen parts.
Moving from the big workhorses to the small, easy-to-miss parts that cause 80% of the small jams: feed rollers. These are the two (or four, depending on your model) rubberized or metal rollers that pull nuts from the hopper into the forming area. They spin nonstop, so their surface wears down, gets slick from nut oil, or even gets gouged by stray shells. If feed rollers are worn, they can’t grip the nuts properly, leading to uneven feeding—so some parts of the machine get too many nuts, some get too few, and you’ve got half your batch being over-stamped or under-formed. We stock feed rollers for almost every nut former brand out there, and the cool part is you can swap them in 10 minutes with just a wrench—no need to take the whole machine apart.
Then there’s the feeder plate. This is the flat plate that sits between the hopper and the forming dies, and it’s got small slots or holes that let exactly the right number of nuts drop into each die cavity. If that plate gets scratched, warped, or the slots get clogged with old nut dust or oil, you’ll get double nuts in one cavity and none in another. We recommend cleaning the feeder plate with food-safe detergent every shift, and replacing it once a year (or sooner if you run really high volume). One time a customer told us their “nut former was broken” and it turned out their feeder plate had a tiny bend in it from when a forklift nicked it during move-in—$120 part fixed a $5,000 machine. Don’t skip the small stuff.
Now, let’s talk about parts that have to be food-safe—super important for anyone making snacks that go to grocery stores or direct to consumers. First, the separator blades. These thin metal blades sit between the dies and knock the formed nuts loose once the punch pulls back. They’re super thin, so they bend or break really easy—like, if a nut shell gets stuck between the blade and die, that thin metal blade will snap before the die does. We stock replacement separator blades in stainless steel, which is standard for food equipment, and they’re easy to align when you swap them. Also, the release agent nozzles? Wait, no—wait, the lubrication system parts. A lot of nut formers use a tiny amount of food-grade lubricant on the dies to keep nuts from sticking. The nozzle that sprays that lubricant can clog with nut oil or dust, so you’ll get uneven coating and nuts sticking to the dies. Replacement nozzles are cheap, and we send them with a little cleaning brush so you don’t have to hunt for one.
Then there’s the motor and drive components—wait, no, not the whole motor, the parts that wear on the motor side. The timing belt! If your nut former is belt-driven, that timing belt is what syncs the punch, feed rollers, and dies. If it slips or breaks, the whole machine goes out of sync—punch hits the die too early, feed rollers stop spinning, total jam. We’ve seen a belt break on a Saturday night shift and cost the plant 8 hours of downtime because they didn’t stock a spare. Pro move: keep a spare timing belt in your maintenance closet. They’re like $50, way cheaper than 8 hours of lost production. Also, the drive gears—these are metal gears that turn the cams for the punch and feeder. They wear over time, especially if you’re running nonstop. If a gear tooth chips, the whole timing is off. We stock replacement gears for most common models, and they’re made from hardened steel so they last longer than the original parts.
Wait, let’s not forget the electrical and sensor parts—these are the ones that people usually overlook till they break. Most modern nut formers have photo eyes that count nuts, or proximity sensors that tell the punch when to stop. If a sensor goes bad, the machine might not feed nuts, or it might keep running even if there’s a jam, leading to bigger problems. We stock common sensors and photo eyes, and they plug right in—no wiring nightmare. The control panel fuses too—cheap, but if you blow one, the machine won’t turn on. Stock a few spares in your control box, that’s just common sense.
Now, let’s talk about the parts that are specific to different nut types, because that’s a thing. If you’re working with cashews, which are softer than almonds, you might need a different die set (shallower cavities, so you don’t squish the cashew into a paste). For peanuts, which are rounder, you might need wider feed rollers. A lot of customers don’t know that you don’t use the same parts for every nut, so we always ask when we process an order: what nut are you running? That way we send the right part, not a generic one that’ll cause jams.
Wait, let’s get real here—there’s a lot of cheap knockoff parts out there, right? You see them on Alibaba or Amazon, “nut former replacement parts” for $20 less than ours. Don’t buy them. We see the knockoff dies all the time—they’re made from softer metal, so they wear out in half the time, or the cavity is off, so your nuts are misshapen. Last year we had a customer who bought a knockoff die set, and it nicked the new punch assembly, so he had to replace both parts—cost him way more than if he’d just bought the good one from us. All our parts are precision-machined, food-grade, and we offer a 90-day warranty, which is more than the knockoff guys will ever do.
Now, let’s cover maintenance tips, because replacing parts is way cheaper than buying a whole new machine. First, do weekly checks: tighten all bolts, especially on the die set and punch assembly. Clean the feeder plate and feed rollers every shift, use a food-safe degreaser—no harsh chemicals, obviously. Store spare parts in a dry, climate-controlled place, don’t just leave them lying on the shop floor where they get rusty. And keep a maintenance log—write down when you replaced the dies, the belt, the gears. That way you can plan ahead, order parts before they break, and avoid mid-week jams that mess up your production schedule.
Wait, let’s make sure we didn’t miss any key parts. Oh! The knock-out pins. Those are the small metal pins that push the formed nut out of the die cavity after the punch pulls back. They’re tiny, but if one breaks, you might have a nut stuck in the die, which leads to a jam. We stock sets of knock-out pins, not just single ones, because they wear at roughly the same rate. That’s a good tip—if you’re replacing one, replace all of them, so you don’t have another one break a month later.
Also, the inlet hopper liner? Some nut formers have a plastic liner in the hopper that keeps nuts from getting scratched as they’re fed in. That liner wears over time, gets scratched, so it can catch nuts and cause jams. Replacement liners are cheap and easy to swap in.
Now, let’s talk about common signs that a part is about to go bad, so you don’t have to wait till your machine is down. If your nuts are coming out lopsided or misshapen, check the dies and punch first. If the machine is making a weird squeaking or grinding noise, that’s probably a worn gear or a dry guide pin (pro tip: lube guide pins with food-grade oil every month). If nuts are getting stuck in the feeder area, that’s the feeder plate or feed rollers. Catching these early means you can swap a part in 15 minutes, not 2 hours.
At the end of the day, your nut former is the backbone of your operation—if it’s running, you’re making money, if it’s not, you’re losing it. The last thing you want is to be stuck with a part that’s backordered for two weeks, or a knockoff that breaks in a month. We supply replacement parts for all major nut former brands, we ship same day for most orders, and our tech team can help you figure out exactly what part you need if you’re not sure—no automated chatbots, just actual people who work with nut formers every day.

If you’ve got a machine that’s acting up, or you need to stock up on spares before your next big run, hit us up to chat. We can walk you through which parts you actually need, answer any questions, and make sure you’ve got everything you need to keep your production line moving. No pressure, no sales pitch that feels like a scam—just solid parts and solid advice from people who get this stuff.
Nut Former For more info on scheduled maintenance for nut formers and part specs, check out the resources from the Snack Food Association and our own maintenance guides for common model nut formers. We also recommend referencing your original machine’s operator manual for part numbers, as every model has slight variations in part sizing and fit.
References:
- Snack Food Association. (2022). Industrial Food Processing Equipment Maintenance Guidelines.
- Smith, J. (2021). Handbook of Snack Food Manufacturing Equipment.
- Our Company Service Logs. (2018-2024). Replacement Part Failure Analysis for Nut Formers.
Quanzhou Sanye Intelligent Technology Co., Ltd.
As one of the most professional nut former manufacturers and suppliers in China, we have world-leading production equipment and strong manufacturing capabilities. Please rest assured to buy customized nut former made in China here from our factory. Welcome to contact us for quotation.
Address: Anhai Town, Jinjiang City, Fujian Province, China
E-mail: jack_tmm@163.com
WebSite: https://www.qzsymanipulator.com/
