If you’ve ever watched a grinding machine shape a block of metal into a precise component for an engine, a medical device, or even a aerospace part, you might not stop to think about how the grinding parts themselves hold up under that extreme friction and pressure. As someone who’s been supplying grinding parts for 12 years, I’ve seen first-hand how choosing the right material can make the difference between a part that lasts 6 months and one that runs flawlessly for 5 years. Today, I want to break down the most common materials we work with, why each matters, and what you need to know to pick the right one for your grinding application. Grinding Parts

First, let’s set a quick context: grinding parts are the components that do the cutting, shaping, or finishing work in a grinding machine. That includes grinding wheels, abrasive grains, bond materials, even the small pins or discs used in precision micro-grinding. Each material is chosen to balance three key things: abrasion resistance (how well it stands up to rubbing against the workpiece), toughness (how little it chips or breaks under pressure), and bond strength (how well the abrasive grains stay attached to the part without falling off too soon. It’s a tight balance, and that’s why material selection isn’t just a technical detail—it’s the backbone of a reliable grinding process.
Let’s start with the most widely used material for general-purpose grinding: aluminum oxide. If you’ve ever grabbed a standard bench grinding wheel, that’s almost certainly aluminum oxide (often shortened to alumina, or Al₂O₃). This material is made by fusing bauxite ore at extremely high temperatures, then crushing it into grits of different sizes. What makes aluminum oxide so popular is its versatility: it’s tough enough to grind steel, iron, and most non-metallic materials without breaking apart, and it’s affordable compared to more specialized abrasives. For example, a customer last year needed wheels to grind structural steel for bridge components—aluminum oxide worked perfectly there, because it can handle the consistent pressure of heavy stock removal without wearing out too fast. We also offer graded aluminum oxide, where smaller grit sizes are used for finishing work, and coarser grits for rough grinding. The one caveat? It’s not the best choice for non-ferrous materials like aluminum or brass, because it tends to clog the grinding wheel’s pores, slowing down the process.
Next up, silicon carbide, another staple in grinding parts. Unlike aluminum oxide, silicon carbide (SiC) is a compound of silica sand and carbon, fused at even higher temperatures. It’s harder than aluminum oxide—about 9.5 on the Mohs scale, compared to alumina’s 9—but it’s also more brittle. That brittleness is actually an advantage for certain jobs: when it does chip, it forms sharp, new edges instead of dulling, so it maintains its cutting ability longer. Silicon carbide is the go-to for grinding hard, non-metallic materials: stone, glass, ceramics, and even semi-conductor materials like silicon wafers. Last quarter, a client in the tile manufacturing industry needed parts to grind glazed ceramic tiles—silicon carbide was ideal here because it cuts evenly without leaving scratch marks, and it resists clogging on the smooth, dense tile surface. It’s also used for grinding cast iron, where its hardness helps break down the hard surface of the metal. The downside? It’s not as tough as aluminum oxide, so it’s not for heavy stock removal. If you tried to use a silicon carbide wheel to grind thick steel, it would likely crack or wear away in days, not months.
Then there’s diamond, the king of hard materials, and a grinding part we supply heavily for high-precision, tough jobs. Natural diamonds are rarely used for grinding parts today—they’re too expensive and inconsistent—so almost all industrial diamond grinding parts are made from synthetic diamond, grown in controlled labs to have uniform hardness and size. Synthetic diamond is 10 on the Mohs scale, the hardest material known, and it’s the only abrasive that can grind extremely hard materials like tungsten carbide, hardened steel, and carbide tooling. A recent example: a tool and die maker came to us needing grinding parts for shaping carbide drill bits—their old parts wore out after a week, but diamond parts last 10 times longer. The key here is that diamond doesn’t react with carbide, unlike some other abrasives that can cause chemical wear. The trade-off is cost: diamond grinding parts are 3 to 5 times more expensive than aluminum oxide, so you only use them when you need that extreme hardness, or when the material being ground is so hard no other abrasive will work. We also offer plated diamond parts, where a thin layer of diamond is bonded to a metal backing, which is perfect for small, precision jobs like grinding surgical tools.
Another specialty material is cubic boron nitride, or CBN. If diamond is for grinding hard carbides, CBN is for grinding hardened steels—think gears, bearings, and automotive engine components. CBN is a man-made material, developed in the 1950s, and it’s second only to diamond in hardness, but it has a unique advantage: it doesn’t react with iron, unlike diamond, which can cause unwanted chemical changes in ferrous metals. That makes CBN the ideal choice for high-speed grinding of hardened steel, where heat buildup is a big risk. A customer in the automotive industry reached out last year because their old grinding wheels were overheating and causing warping in transmission gears. We supplied CBN grinding wheels, which run cooler, cut faster, and last longer than aluminum oxide wheels for that application. CBN parts are also more expensive than aluminum oxide, but they pay for themselves in reduced downtime and better part quality. We offer both solid CBN wheels, used for heavy grinding, and plated CBN parts, for precision finishing work.
Now, let’s talk about the bond material, which is just as important as the abrasive itself. The bond holds the abrasive grains in place, and it wears away gradually to expose new, sharp grains as the old ones dull. There are four main bond types we work with, and each pairs with a specific abrasive and application. Resin bonds are the most common—they’re made from phenolic or epoxy resin, which is flexible, so they absorb shock, making them perfect for heavy stock removal. Vitrified bonds are ceramic, hard and porous, which allows for good heat dissipation, so they’re ideal for precision grinding. Metal bonds are made from bronze or nickel, very strong, used with diamond or CBN for heavy-duty, high-speed applications. And rubber bonds, flexible, used for polishing and finishing jobs, like grinding precision lenses or delicate metal parts.
I get a lot of questions from customers about when to choose one material over another, so let’s run through a quick cheat sheet. If you’re grinding mild steel, iron, or general metal parts, go with aluminum oxide. If you’re grinding glass, stone, ceramics, or aluminum, pick silicon carbide. If you’re grinding carbide, hardened steel, or high-precision tooling, go with diamond or CBN. It’s also worth noting that the size of the abrasive grain matters: coarser grains (36 to 60 grit) are for rough grinding, when you need to remove a lot of material fast, and finer grains (120 to 600 grit) are for finishing, when you need a smooth, precise surface.
Over the years, I’ve seen customers make mistakes with material selection all the time. Once, a small machine shop came to us with a silicon carbide wheel they were using to grind thick steel shafts. It worked for a week, then cracked and broke, costing them a day of production. We recommended aluminum oxide instead, and that wheel lasted 6 months, saving them thousands in replacement costs. Another time, a glass manufacturer tried aluminum oxide wheels for grinding their products, and the wheels clogged immediately, slowing down their line. Switching to silicon carbide fixed that, no more downtime. Those experiences taught me that there’s no one-size-fits-all material in grinding parts—getting it right depends on your workpiece, your machine, and your end goal.
We also work with custom grinding parts, so if you have a unique application, we can help you pick the right material and bond to meet your needs. Whether you’re a small shop grinding parts for a hobby, or a large manufacturer working on aerospace components, we have the expertise to guide you.
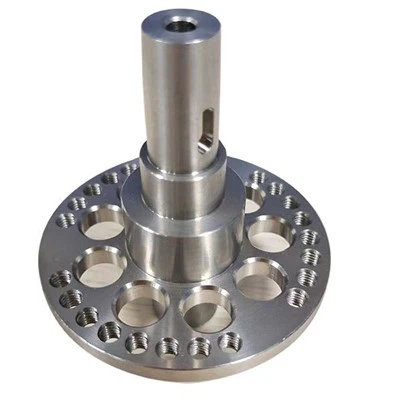
If you’re looking to replace your current grinding parts, or if you’re starting a new project and need to pick the right material, don’t hesitate to reach out to our team to discuss your requirements. We’ll walk you through the pros and cons of each option, share case studies from similar applications, and make sure you get parts that perform reliably and fit your budget.
Automation Parts References:
- “Abrasives and Grinding Wheels,” American Society of Mechanical Engineers (ASME) B74.1, 2017.
- Chemical Composition and Performance of Industrial Abrasives, Industrial Diamond Association of America, 2020.
- Bond Materials for Grinding Tools, Society of Manufacturing Engineers (SME) Technical Paper, 2019.
- Machining Hardened Steels with CBN Abrasives, International Journal of Machine Tools and Manufacture, Vol. 50, No. 12, 2010.
Suzhou Huaquan Electromechanical Manufacturing Co., Ltd.
As one of the leading grinding parts manufacturers in China, we warmly welcome you to buy bulk customized grinding parts made in China here from our factory. If you have any enquiry about pricelist and free sample, please feel free to email us.
Address: No.7550 Mudong Road, Hengjing Town, Wuzhong District, Suzhou City, Jiangsu Province, China
E-mail: Huaquan2005@outlook.com
WebSite: https://www.huaquancnc.com/
